

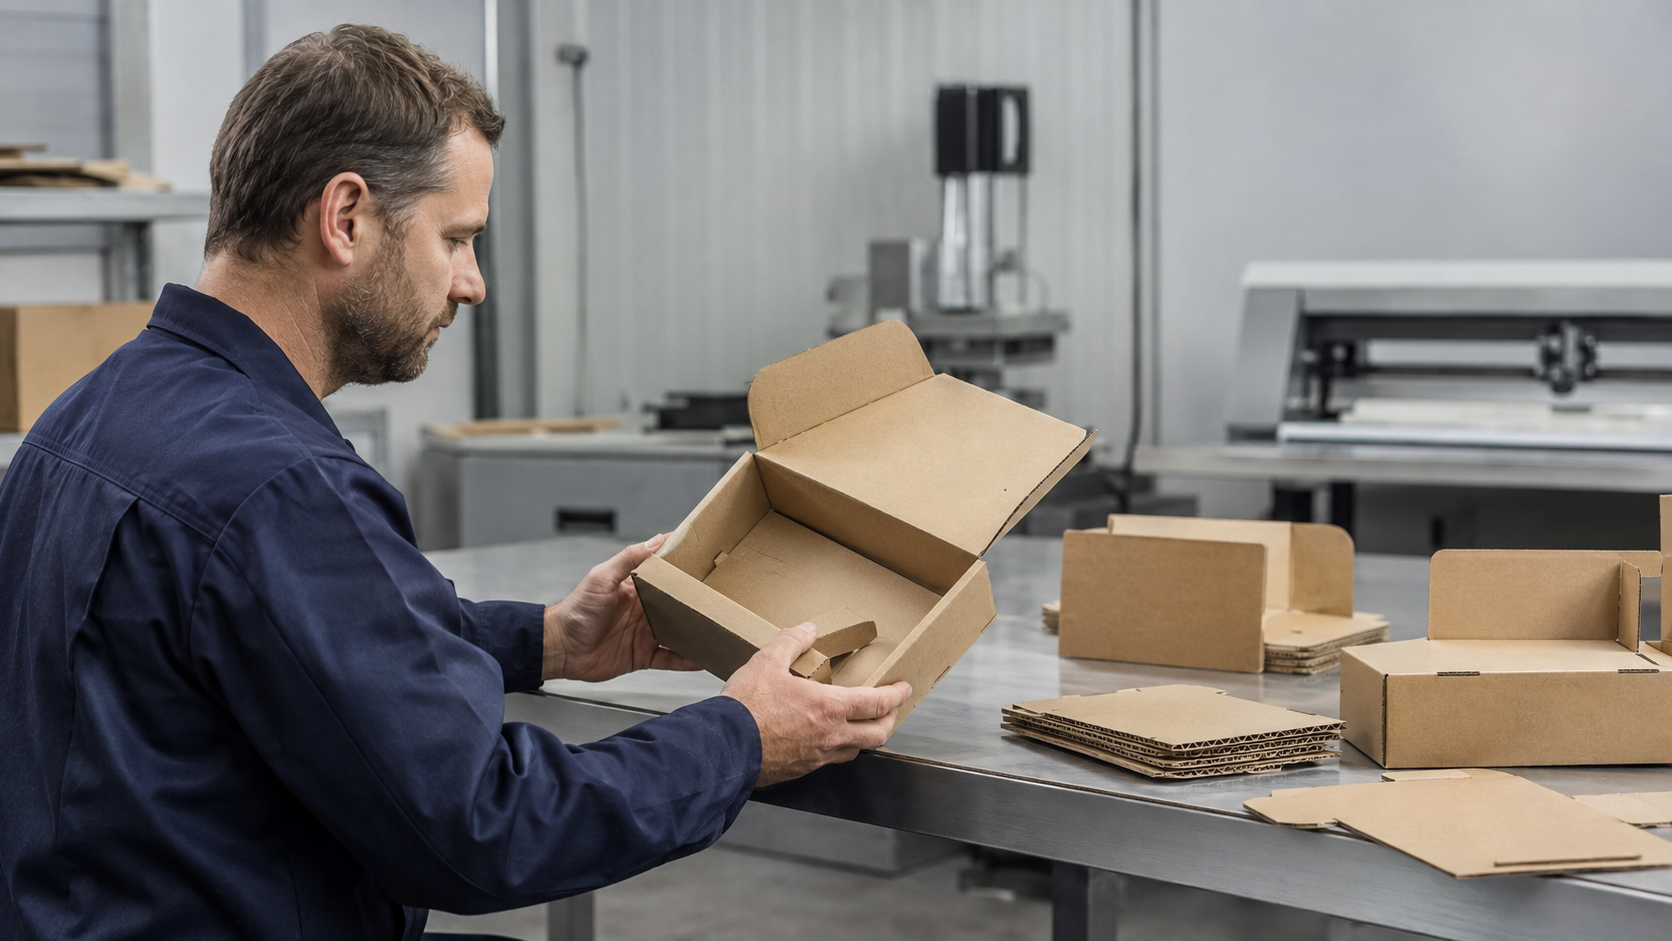
Damage in courier shipments rarely has a single cause. The result depends on box construction, corrugated board, empty space, product stabilization, closure quality and repeatability at the packing station. Reducing complaints therefore requires a review of the complete system, not only a stronger carton.
Good packaging should absorb external loads, keep the product away from exposed walls and corners and prevent movement. At the same time, it has to remain practical for operators and economical at the planned volume.
Quick answer: how can courier damage be reduced?
The strongest improvement usually comes from five connected actions:
- classify recurring damage types and where they occur,
- match the box dimensions to the product or order basket,
- immobilize the product with a purposeful insert or divider,
- select board and construction for product weight and distribution,
- verify the prototype through testing and a controlled shipping pilot.
Adding more void fill is not a complete solution. Loose material can shift, compress or leave the product next to a wall. Protection should come from packaging geometry and known risk scenarios.
Where should a damage review start?
Start by structuring the evidence. A photograph of a damaged product without information about the box, insert and route has limited value. Record the SKU, packaging format, carrier, date, damage type and location of package failure for every incident.
A useful classification includes crushing, puncture, breakage, scratching, leakage, component movement, closure opening and corner damage. After several dozen cases, a pattern often becomes visible. The team can then design against the real problem instead of strengthening every component without direction.
What loads does a courier parcel experience?
A parcel is handled repeatedly, transferred across conveyors, stacked and compressed by other shipments. It may fall on a face, edge or corner. Vehicle vibration can gradually move the product, while humidity and temperature changes can reduce corrugated-board performance.
It is impossible to predict every event, but packaging can be designed for the most likely scenarios. Lightweight apparel has different priorities from glass jars, cosmetic sets or high-value electronics.
Right-sizing: less empty space, more control
An oversized box allows the product to build momentum before striking a wall. It also needs more fill, which may not remain in place. Packaging that is too tight can transfer impact directly to the product and leave no protective clearance.
Internal dimensions must account for the product, insert, loading method and production tolerances. For a broad SKU portfolio, packing groups are often more practical than one box per item. Dimensional variation must not defeat the stabilizing function.
Product stabilization: an insert instead of random void fill
A corrugated insert can block movement in three axes, separate multiple items, protect pumps and closures and hold the product away from corners. It should be intuitive to assemble and difficult to install incorrectly.
Support points are critical. They must not load fragile components, buttons, cables, bottle necks or decorative surfaces. At the same time, the insert cannot be so loose that repeated vibration releases the product.
Loose fill still has a role in irregular baskets, but quantity and application should be defined. In a repeatable process, a purpose-designed construction usually provides more control and faster packing.
Selecting corrugated board for load and distribution
The number of layers alone does not define performance. Paper properties, flute combination, flute direction, box dimensions, construction and use conditions all matter. A package may need compression, puncture or impact resistance, or tolerance to reduced strength under humidity.
BART works with 2-, 3-, 5- and 7-layer board and F, E, B and C flutes. Selection should follow the product and supply chain rather than habit. Projects can be supported with ECT, FCT, BST, BCT and Cobb testing. See BART’s research and technology capabilities.
Box construction and closure
A regular slotted carton is versatile, but its performance depends on correct sealing and control of empty space. A die-cut construction can integrate stabilization, adhesive strips and controlled opening. For heavy products, the base and load path also require attention.
Closure must remain effective despite board stress, dust and changing conditions. Tape should match the board surface and application temperature. An integrated adhesive strip can reduce process variation, but it also requires validation with the final material and storage time.
Laboratory tests and distribution trials
Material testing helps compare options and control repeatability, but it does not replace assessment of the complete package. BCT indicates box compression performance, while drop, vibration or controlled shipping trials evaluate the product-packaging system.
The test scope should be proportional to risk. A light, resilient product does not need the same protocol as glass or electronics. Conditions, pass criteria and sample configuration must be recorded so future results can be compared.
Packing instructions are part of the design
Even a strong construction can fail if an operator selects the wrong format, reverses an insert or omits a component. Instructions should be short, visual and available at the workstation. Define folding sequence, product position, additional material, closure and label location.
Observe operators during the pilot rather than relying only on feedback. Extra movements, searching for orientation or correcting creases reveal error risk before volume increases.
A seven-step implementation plan
- Collect damage data and photographs from a representative period.
- Select priority SKUs, baskets and delivery channels.
- Define protection criteria and an acceptable total parcel cost.
- Prepare structural and material prototypes.
- Run workstation and technical tests appropriate to the risk.
- Launch a controlled shipping batch and monitor claims.
- Approve the specification, packing instruction and control plan.
Common mistakes
- strengthening the box without identifying the failure mechanism,
- adding fill instead of immobilizing the product,
- testing an empty box without the final product,
- ignoring external dimensions and shipping cost,
- failing to standardize packing instructions,
- rolling out full volume without a pilot.
Damage reduction should also improve operational cost. Monitor claims together with packing time, material use and shipping. The broader model is explained in our guide to the total cost of e-commerce packaging.
FAQ
Does stronger corrugated board always reduce damage?
No. If the product moves or is supported in the wrong place, stronger box walls may not solve the problem. Identify the damage mechanism first.
How much clearance should surround the product?
Enough for the designed protective zone and insert. There is no universal value. Clearance must not allow free movement, while exposed product areas should remain away from vulnerable walls and corners.
Is BCT enough for courier packaging?
BCT is important for compression, but it does not show the complete response to drops, impacts or vibration. The program should match product and channel risks.
How long should a shipping pilot run?
It should include enough parcels to compare with the baseline damage rate and cover representative routes and baskets. A low baseline claim rate requires a larger sample.
When should the packaging producer be involved?
Before dimensions and process are frozen. Early collaboration connects protection, materials, packing cost and production requirements.


